As semiconductor manufacturing processes continue to advance, the purity requirements for wet electronic chemicals keep rising, and so do the performance standards for their packaging containers. In critical processes such as cleaning, wet etching and post-CMP cleaning, Ultra-Clean HDPE Drum serves as key packaging for the storage and transport of wet electronic chemicals. Its purity control, chemical resistance, temperature resistance and long-term storage stability directly affect chemical quality and wafer yield. For high-risk and highly corrosive chemicals such as high-purity hydrochloric acid and hydrofluoric acid, packaging, storage and transport are subject to even stricter requirements.
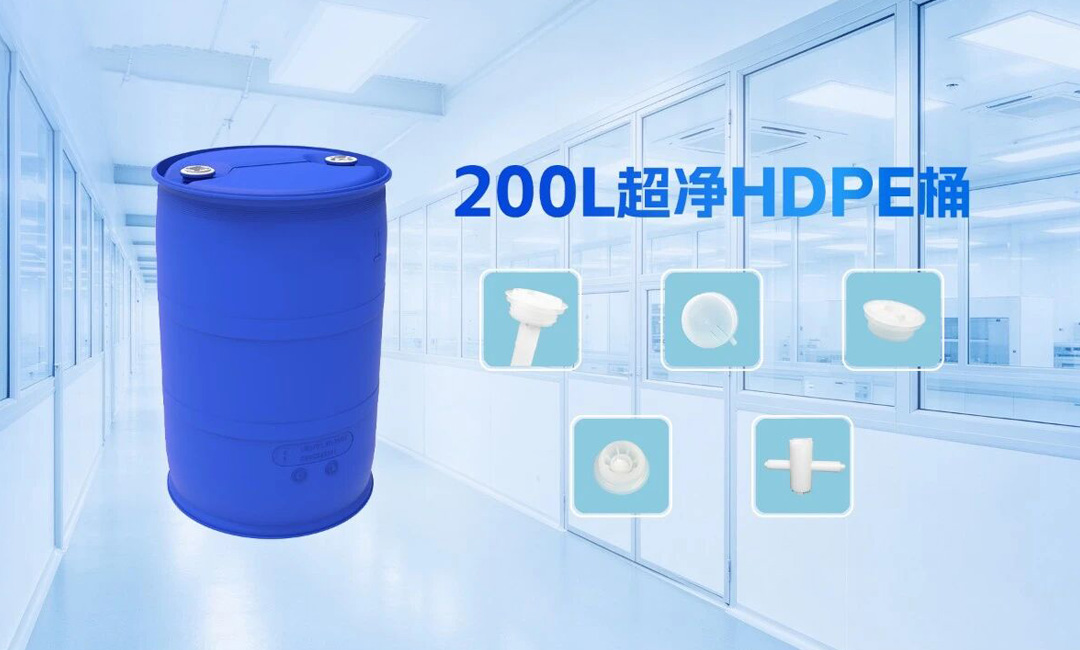
Designed for the storage and transport scenarios of high-purity chemicals, BSL Ultra-Clean HDPE Drum delivers a practical packaging solution for electronic chemicals in semiconductor manufacturing, precision electronics and other industries.
Rigorous Full-Scale Testing to Secure the Safety of High-Purity Storage & Transport
BSL Ultra-Clean HDPE Drum undergoes comprehensive strict tests covering physical properties and chemical leachables. Validated by long-term immersion tests, the leaching level of individual metallic impurities from the drum body can be controlled below 10 ppt. Its particle count, UV transmittance and other parameters reach industry-leading benchmarks, meeting the requirements for Grade G5 electronic chemicals. In terms of physical safety, the drum is certified to UN 1H1/Y1.9/170. The drum opening adopts a high-sealing design to safeguard leak control and structural integrity during hazardous goods transportation and industrial warehousing.
Complete Accessories for Diverse High-Purity Chemical Applications
Chemical storage and transport involve varied operating conditions with different accessory requirements. BSL Ultra-Clean HDPE Drum supports a full accessory portfolio including liquid dispensing caps, standard caps and vented caps.
For instance, liquid dispensing caps are used to transfer liquid from the drum to external pipelines when chemicals need to be pumped and delivered through tubing. BSL has optimized the mating structure between liquid dispensing caps and pipelines to reduce dripping and leakage during pumping and transfer. For volatile chemicals or pressure-sensitive materials, temperature fluctuation or stacking load may trigger internal pressure changes. Vented caps balance internal and external pressure differentials, lowering the risk of drum bulging under positive pressure or collapse under negative pressure, and supporting stable storage and transport.
Diverse Sizes to Fit Global Application Scenarios
Industry standards, chemical properties and operating conditions vary across regions. Drums of the same specification may require different connection methods and operating requirements on different production lines. BSL offers the standard 200L size to meet general industrial production and logistics needs, with metric and NPT (US standard) models compatible with manufacturing sites worldwide.
Consumption of high-purity chemicals continues to grow, and packaging containers are taking on an evolving role in the supply chain, gradually becoming a critical factor governing chemical quality. Covering drum bodies, accessories and specifications, BSL expands its product lineup around high-purity chemical packaging demands, tightly controls key performance metrics, and provides customers with long-term packaging solutions.